
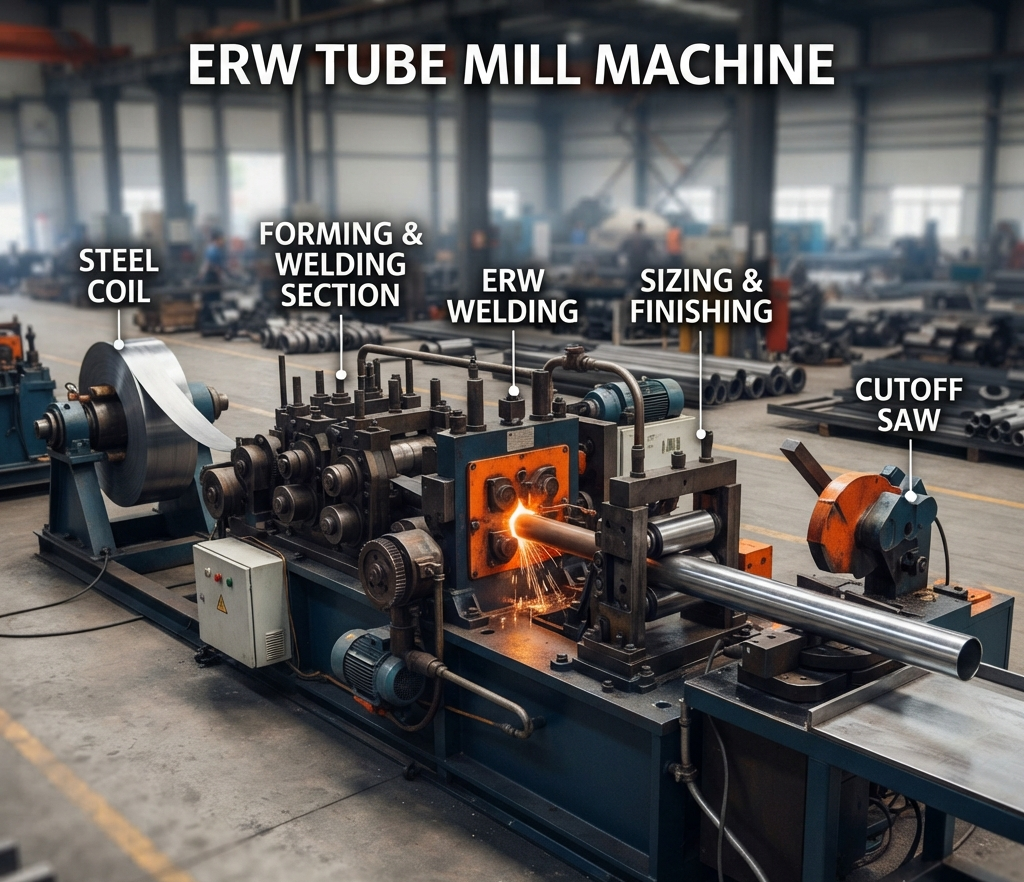
Steel tubing supports everything from furniture frames and automotive components to structural assemblies and fluid-handling systems. Reliable output depends on precise forming, welding, and sizing. Understanding the differences between a Tube Mill Machine and an ERW Tube Mill Machine supports practical equipment planning.
What Is a Tube Mill Machine?
A Tube Mill Machine is an integrated production system that converts metal strip into continuously formed, typically welded tubing. Roll stands gradually bend the strip, while downstream stations join, size, straighten, and cut the finished product. Tooling determines available profiles.
Buyers should assess materials, tolerances, tooling, and realistic throughput.
Wall thickness and diameter should be evaluated together: a line capable of one large diameter may not support every thickness within that nominal range.
What Makes an ERW Tube Mill Machine Different?
An ERW Tube Mill Machine is a specific welded-tube production line using electric resistance welding principles. In common high-frequency ERW systems, electrical energy heats the strip edges and squeeze rolls forge them together, generally without added filler metal.
Weld quality depends on precise alignment, edge preparation, pressure, material, and electrical settings.
Understanding the Welding Stage
Strip edges form a controlled V before heating and squeezing create the seam.
Why Edge Preparation Matters
Clean, even edges and stable tracking support reliable seams.
How the Production Process Works
Although layouts differ by equipment supplier, a typical welded-tube line follows these stages:
-
Uncoiling: Strip steel unwinds from a coil into the production line.
-
Joining and accumulation: Coil ends are connected, while an accumulator may maintain continuous mill operation.
-
Forming: Successive rollers gradually shape the flat strip into an open tube.
-
Welding: The approaching edges are joined using the mill’s specified welding technology.
-
Bead treatment: The external weld bead is removed or finished when required.
-
Cooling and sizing: Controlled cooling precedes precise dimensional adjustment.
-
Straightening and cutting: Tubes are aligned and cut into specified lengths.
-
Inspection: Suitable tests verify dimensions, surface condition, and seam integrity.
A bottleneck at any stage limits overall output.
Essential Components and Their Functions
Key assemblies include:
-
Uncoiler and accumulator: Manage strip feeding and reduce interruptions between coils.
-
Forming stands: Shape the strip progressively without excessive distortion.
-
Welding assembly: Supplies the intended energy and joining pressure.
-
Sizing stands: Bring the profile closer to its target geometry.
-
Cutoff unit: Produces repeatable lengths with suitable line synchronization.
-
Control system: Coordinates motors, operating parameters, and fault indications.
Options include automated handling, bead removal, and weld inspection.
Tube Mill Machine vs ERW Tube Mill Machine
|
Comparison point |
General tube mill line |
ERW tube mill line |
|---|---|---|
|
Main description |
Broad category of tube-forming equipment |
Tube mill configured for electric resistance welding |
|
Joining method |
Depends on machine design |
Resistance-based seam welding, often high frequency |
|
Typical output |
Formed tube profiles, according to tooling |
Continuously welded steel tubes and profiles |
|
Critical setting |
Forming accuracy and selected joining process |
Forming accuracy plus heat and squeeze control |
|
Selection priority |
Product geometry and line architecture |
Material suitability and welded-seam requirements |
ERW is a type of tube mill, not a separate category of manufacturing.
How to Choose the Right Equipment
Before investing in an ERW Tube Mill Machine, define the products the factory must deliver. A practical equipment checklist includes:
-
Material grades: Identify applicable steel grades, coatings, and forming behavior.
-
Tube dimensions: Confirm outside diameter, wall thickness, profiles, and tolerance requirements.
-
Production volume: Match realistic order patterns with operating speed and changeover time.
-
Tooling flexibility: Evaluate roll changes, setup labor, and future product expansion.
-
Inspection needs: Specify suitable dimensional checks and weld-integrity testing.
-
Service support: Review operator training, spare parts, documentation, and maintenance accessibility.
During supplier discussions, verify power requirements, floor space, guarding, and the ability to integrate testing equipment. Clarify whether claimed capacity reflects sustained production or demonstration runs.
For regulated applications, define the applicable product standard before buying machinery. Inspection frequency, mechanical properties, traceability, and required seam treatment may influence the planned line specification.
Request trials with intended materials and tube sizes.
Improving Output Without Sacrificing Quality
Maintain roll alignment, monitor welding, and inspect finished lengths.
Track scrap, downtime, variation, and changeovers. These indicators help identify tooling wear, material issues, and unstable processes. Maintain equipment rather than exceeding validated operating limits.
Frequently Asked Questions
1. What does a tube mill machine produce?
It produces formed metal tubes or hollow profiles, commonly using continuous strip-fed welded production.
2. What does ERW stand for?
ERW means electric resistance welding, a process that joins prepared metal edges through electrical heating and applied pressure.
3. Is every tube mill an ERW line?
No. Tube mill is a broader equipment category; the joining system depends on the line’s design.
4. Does ERW welding need filler wire?
Common high-frequency ERW tube production does not use filler wire.
5. Can these machines make square tubes?
Yes, appropriately equipped lines can produce square and rectangular profiles, sometimes through downstream reshaping.
6. Which materials suit an ERW mill?
Many carbon-steel and selected alloy-steel grades are used, subject to machine capability and process qualification.
7. What determines production speed?
Material, dimensions, weld stability, tooling, cutting capacity, and inspection requirements all influence practical output.
8. Why is roll alignment important?
Correct alignment supports consistent shaping and reduces dimensional errors, edge mismatch, and unnecessary tooling wear.
9. How is weld quality checked?
Methods may include visual inspection, dimensional verification, and qualified nondestructive testing based on applicable standards.
10. What should buyers request from suppliers?
Request operating ranges, utilities, layout drawings, tooling details, acceptance criteria, training arrangements, and support terms.

Leave a Reply